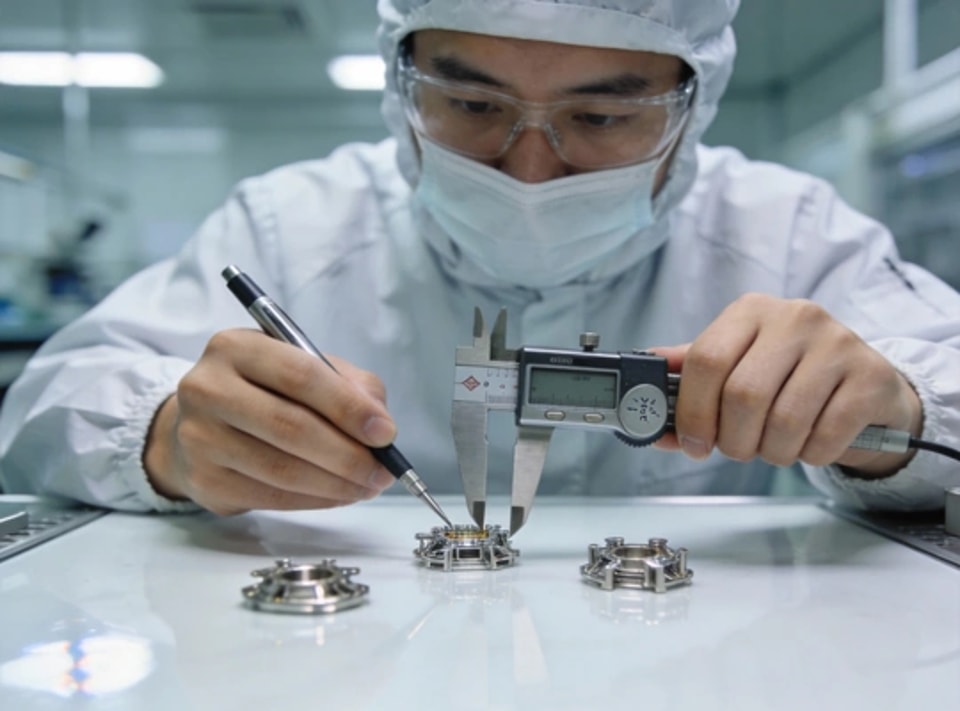
Templates29 is proud to announce the successful achievement of AS9100D certification, the internationally recognized quality management standard for the aerospace industry, following a rigorous 12-month preparation and audit process conducted by TUV Rheinland.Certification ScopeCNC machining of aerospace-grade aluminum, titanium, and nickel alloys5-axis complex geometry machining for structural and engine componentsFirst Article Inspection (FAI) per AS9102 standardFull material traceability from raw stock to finished componentInvestment in QualityTo support this certification, Templates29 invested $2.5 million in new quality infrastructure including:Zeiss Contura G2 CMM with VAST XTR gold scanning probeDedicated aerospace cleanroom inspection area (Class 100,000)Upgraded ERP system with lot-level traceability and ITAR-compliant data handlingComprehensive training program for all 45 production staff members"AS9100D certification represents our commitment to the highest quality standards in precision manufacturing. This milestone enables Templates29 to serve Tier 1 and Tier 2 aerospace suppliers with confidence." - Quality Director, Templates29
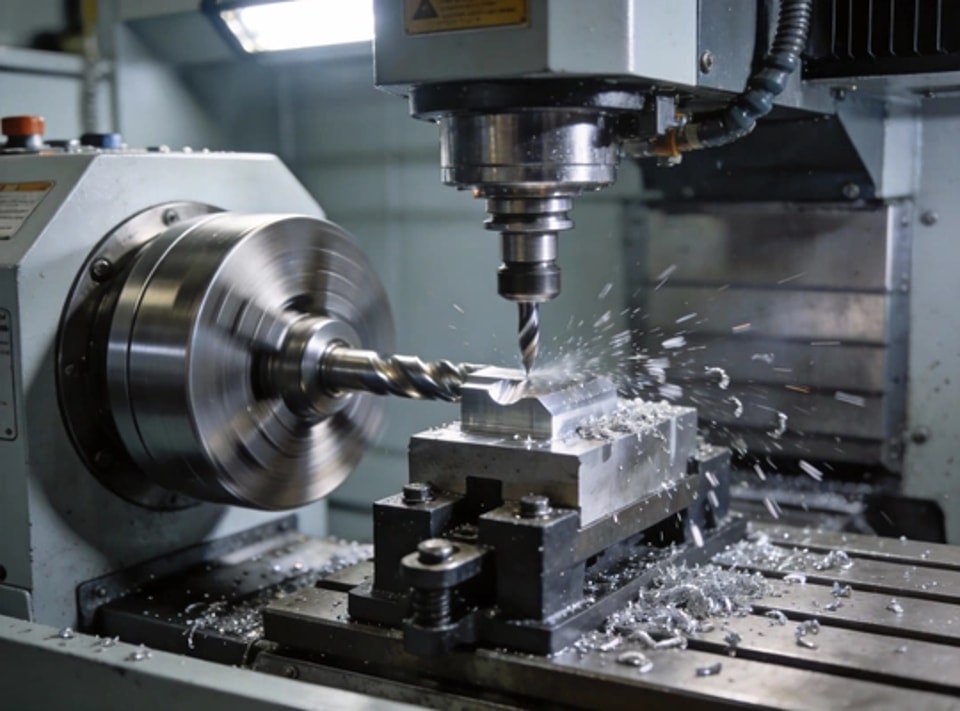
Templates29 expands our precision machining capabilities with the addition of three DMG Mori DMU 65 monoBLOCK 5-axis simultaneous machining centers, enabling production of complex aerospace and medical components previously requiring multiple setups.New CapabilitiesSimultaneous 5-axis: Full contouring capability for impellers, turbine blades, and freeform surfacesHigh-speed spindle: 20,000 RPM HSK-A63 spindle for fine finishing of aluminum and titaniumAutomation: Integrated Erowa Robot Compact 80 pallet system for 72-hour unmanned operationAccuracy: Volumetric accuracy Materials QualifiedAluminum: 6061-T6, 7075-T6, 2024-T3Titanium: Ti-6Al-4V (Grade 5), CP Grade 2Nickel alloys: Inconel 718, Inconel 625Stainless steel: 17-4PH, 15-5PH, 316LApplication ExamplesEarly projects include satellite structural brackets (7075-T6, ±0.015mm), medical implant guide plates (Ti-6Al-4V, Ra 0.4μm), and turbocharger compressor wheels (Inconel 718) demonstrating the versatility and precision of our new 5-axis cell.
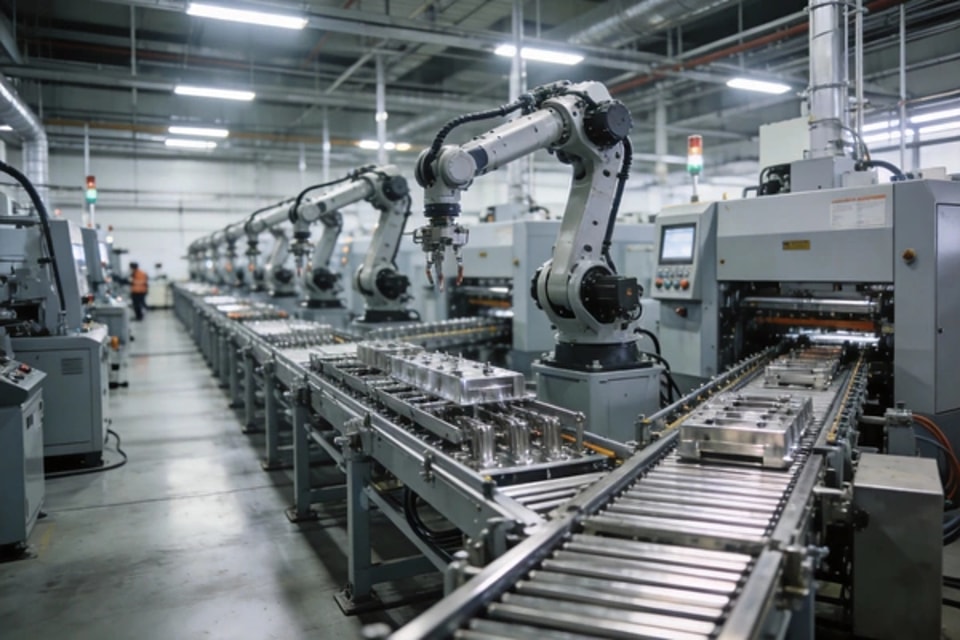
Templates29 announces the grand opening of our new 10,000m² smart manufacturing facility, representing a $15 million investment in next-generation production capacity and Industry 4.0 technologies.Facility Highlights48 CNC machining centers including 12 new 5-axis machines (DMG Mori, Mazak)Automated material handling with AGV fleet and vertical storage towersReal-time production monitoring via IoT sensors on every machineCentral tool management system with RFID tool tracking and automatic pre-settingSustainability Features500kW rooftop solar installation covering 35% of energy needsClosed-loop coolant recycling system reducing water consumption by 60%LED lighting with occupancy sensors throughout production floorChip recycling program recovering 98% of metal waste for remeltingCapacity ImpactThe new facility doubles our annual production capacity to over 5 million components, with dedicated production cells for automotive, aerospace, and medical device customers. Fully operational from Q2 2026.
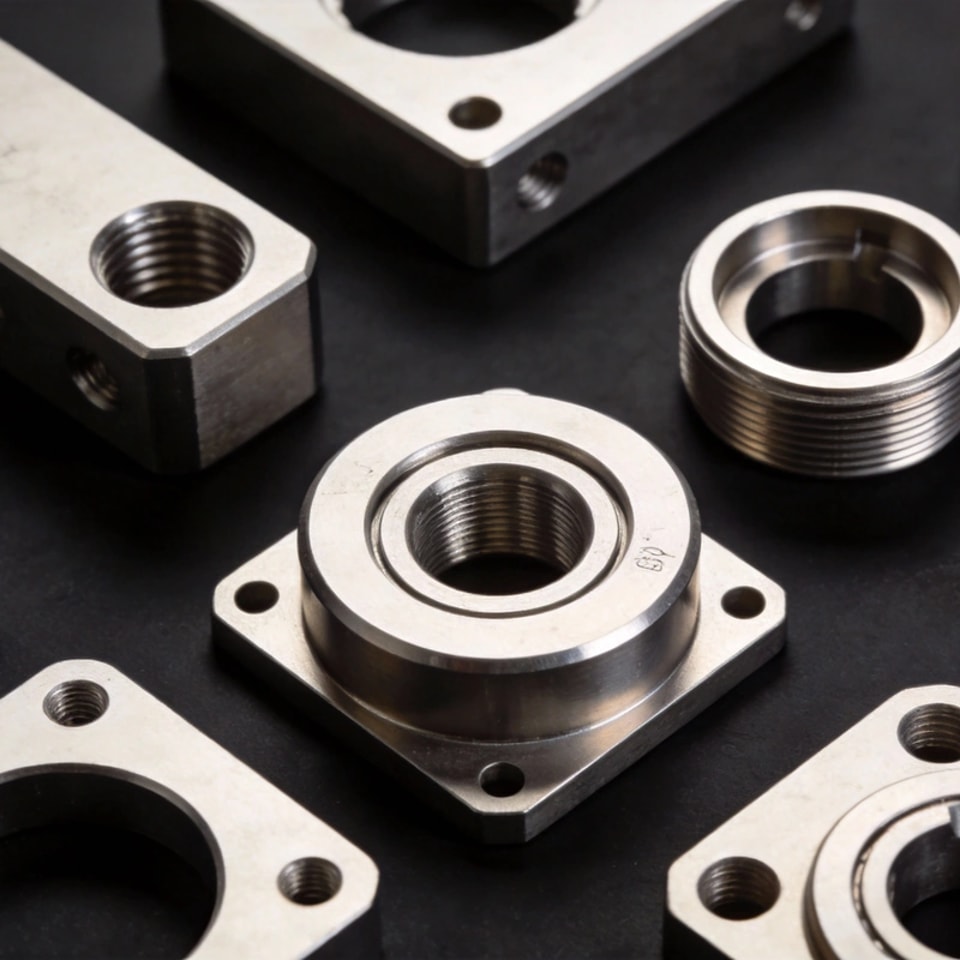
Templates29 announces the installation and commissioning of a new Toshiba DC2000J-GS 2000-ton cold chamber die casting machine, significantly expanding our capability to produce large structural aluminum components for automotive and telecommunications industries.Machine SpecificationsClamping force: 2000 tons, supporting projected areas up to 3,200cm²Shot weight: Up to 25kg aluminum per cyclePlaten size: 1,600×1,400mm for large enclosures and structural castingsCycle time: Optimized 45-90 second cycles with real-time process monitoringIntegrated Production CellABB 6-axis robot for extraction, quenching, and trim press loadingBuhler trim press for automated flash removalX-ray inspection station for porosity detection (ASTM E505 Level 2)Spectrometer for real-time alloy composition verificationTarget ApplicationsThe 2000T line is specifically configured for EV battery tray housings, 5G macro base station enclosures, and automotive structural cross-members requiring thin-wall integrity and high mechanical properties in A380 and A356-T6 alloys.
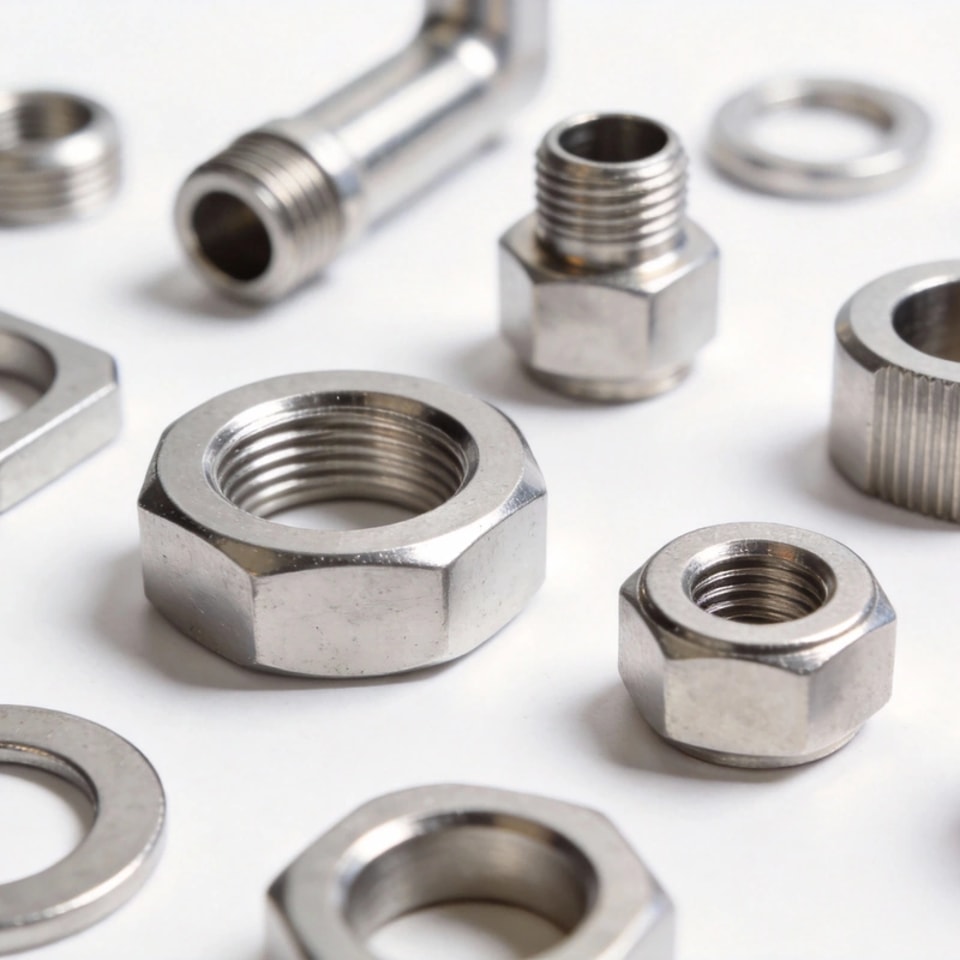
Choosing the right aluminum alloy is critical for achieving optimal performance, machinability, and cost-effectiveness in CNC machined components. This technical guide compares the most commonly specified aluminum alloys and their ideal applications.Alloy Comparison6061-T6 (The Workhorse)Tensile strength: 310 MPa, yield 276 MPaMachinability: Excellent — good chip formation, minimal tool wearWeldability: Excellent — retains 60% strength in HAZ after re-agingBest for: Structural brackets, housings, jigs, fixtures, general machined componentsCost index: 1.0× (baseline)7075-T6 (The Strong One)Tensile strength: 572 MPa, yield 503 MPaMachinability: Very good — requires sharp tools and rigid setupsWeldability: Poor — not recommended for welded assembliesBest for: Aerospace structures, high-stress components, lightweight alternatives to steelCost index: 1.8× (vs. 6061)2024-T3 (The Fatigue Resistant)Tensile strength: 483 MPa, yield 345 MPaMachinability: Good — slightly abrasive, use carbide toolingWeldability: Poor — typically riveted or mechanically fastenedBest for: Aircraft skin, fatigue-critical structural members, fuselage componentsCost index: 1.5× (vs. 6061)Selection Decision MatrixRequirement6061-T67075-T62024-T35052-H32StrengthMediumHighHighLowCorrosionGoodFairFairExcellentWeldabilityExcellentPoorPoorExcellentAnodizingExcellentGoodFairGoodCostLowHighMediumLowDFM TipsSpecify 6061-T6 as default unless specific properties require alternativesFor 7075, design for minimum 2mm wall thickness to avoid distortion during machiningRequest T6 temper for maximum strength; T651 for stress-relieved plate to minimize warpingConsider anodizing compatibility early — 2024 produces inconsistent color in decorative anodize
The global manufacturing landscape is undergoing a fundamental shift as OEMs across automotive, electronics, medical, and industrial sectors accelerate reshoring and nearshoring strategies. This analysis examines the driving forces and implications for B2B component suppliers.Key Drivers of Reshoring1. Supply Chain ResiliencePost-pandemic lessons: 78% of OEMs report increasing domestic supplier diversificationGeopolitical uncertainties driving "China+1" and "China+2" sourcing strategiesInventory carrying costs making shorter supply chains more economically attractive2. Total Cost of Ownership (TCO)Rising overseas labor costs narrowing the cost gap to 8-15% for precision componentsShipping costs stabilized but remain 2.3× higher than 2019 baselineQuality-related costs (scrap, rework, warranty) often 15-20% higher for offshore sourcing3. Government IncentivesCHIPS Act and IRA driving $200B+ in manufacturing investment commitmentsR&D tax credits of 20% for advanced manufacturing processesAccelerated depreciation for capital equipment in reshored facilitiesImpact on SuppliersComponent suppliers positioned for reshoring demand are seeing 25-40% growth in RFQ activity, particularly in CNC machining, die casting, and electromechanical assembly segments. Suppliers with AS9100D, IATF 16949, and ISO 13485 certifications are most in demand.
Surface finish is one of the most frequently specified yet misunderstood parameters in precision manufacturing. This practical guide clarifies surface roughness standards, measurement methods, and achievable values for common machining processes.Key ParametersRa (Arithmetic Average): The most commonly specified parameter — the average deviation from the mean line. Simple and universally understood, but can mask periodic surface patterns.Rz (Average Maximum Height): The average of the five highest peak-to-valley measurements within the sampling length. More sensitive to occasional deep scratches or peaks than Ra.Rmax (Maximum Roughness): The single largest peak-to-valley measurement. Critical for sealing surfaces and bearing bores where worst-case matters.Process Capability ChartProcessRa Range (μm)Typical RaNotesRough turning3.2-12.56.3As-machined, carbide insertFinish turning0.8-3.21.6Fine feed, sharp insertRough milling3.2-12.56.3Face mill, carbideFinish milling0.8-3.21.6Ball nose or wiper insertCylindrical grinding0.1-0.80.4Precision ground journalsSurface grinding0.2-1.60.8Flat reference surfacesLapping0.025-0.40.1Sealing faces, gauge blocksPolishing0.012-0.10.05Mirror finish, opticalCost ImpactEach improvement step in surface finish roughly doubles the processing cost. The jump from Ra 3.2 to Ra 1.6 adds 15-20% cost; Ra 1.6 to Ra 0.8 adds 25-35%; Ra 0.8 to Ra 0.4 adds 40-60% due to grinding requirements. Specify the roughest acceptable finish for each surface to optimize part cost.Drawing Callout Best PracticesSpecify Ra in micrometers (μm) per ISO 1302 or micro-inches (μin) per ASME Y14.36Apply finish symbols only to critical surfaces — leave non-critical surfaces to "as-machined" defaultWhen Rz is critical (sealing faces), specify both Ra and Rz to prevent misinterpretationInclude measurement direction (circumferential vs. axial) for cylindrical parts
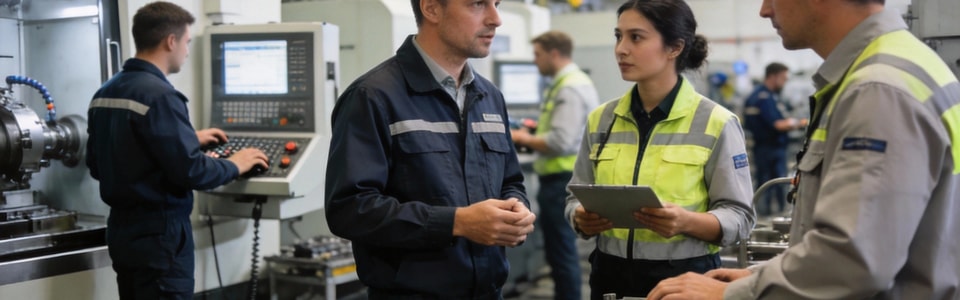
Industry 4.0 is no longer a concept — it is a production reality. This article explores how IoT sensors, digital twin technology, and AI-driven analytics are transforming CNC machining operations from reactive to predictive, delivering measurable improvements in quality, efficiency, and cost.IoT-Connected CNC MachinesVibration monitoring: Accelerometers on spindles detect tool wear signatures 15 minutes before failure, triggering automatic tool changeThermal compensation: Real-time temperature sensors adjust axis positions to maintain ±2μm accuracy during 8-hour production shiftsPower consumption: Current monitoring correlates with cutting forces, identifying optimal feeds and speeds per material-tool combinationDigital Twin BenefitsVirtual commissioning: New part programs simulated with full collision detection before touching real material, reducing first-article scrap by 85%Process optimization: Simulation identifies toolpath inefficiencies, reducing cycle times by 12-18% on averagePredictive maintenance: Component life models predict bearing, ball screw, and way cover replacements 4-6 weeks in advanceROI AnalysisMetricBefore IoTAfter IoTImprovementOEE62%81%+19 pointsScrap Rate3.2%0.8%-75%Unplanned Downtime180 hrs/yr32 hrs/yr-82%Tool Cost$420K/yr$310K/yr-26%Templates29 implemented IoT monitoring across our entire CNC fleet in 2025, achieving payback in 14 months and establishing a foundation for AI-driven autonomous machining optimization.